DfMA in Construction: Design for Manufacture and Assembly
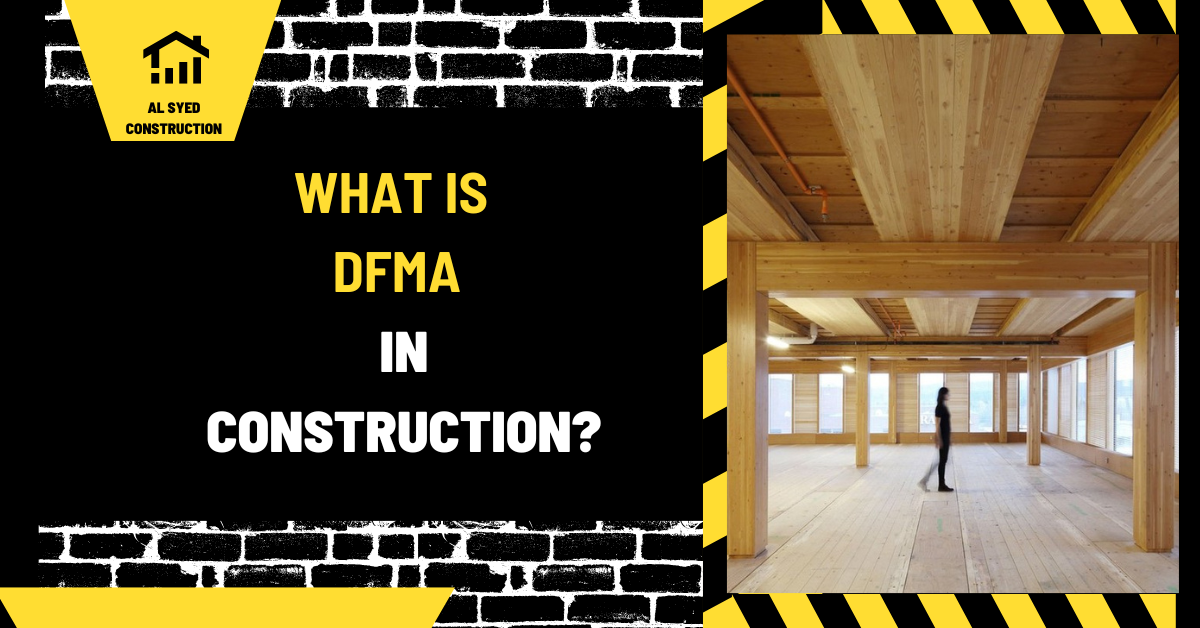
Design for Manufacture and Assembly (DfMA) is a design approach that considers how components will be made and joined while the design is being developed. In construction, it asks architects, engineers, contractors, and manufacturers to simplify and coordinate building elements so they can be fabricated, inspected, transported, installed, and maintained efficiently. DfMA can support prefabrication, but it is not another name for modular construction: a project can use DfMA principles for individual components without using complete room modules.
The aim is not to make every building look alike or to remove architectural judgment. It is to make design choices with a clear understanding of production capabilities and assembly conditions. A good DfMA process keeps the required performance intact while reducing avoidable complexity, rework, access problems, or one-off details.
What DfMA means in a construction project
Manufacture focuses on whether an element can be produced using available materials, equipment, processes, tolerances, and quality controls. Assembly focuses on how elements are handled, positioned, connected, inspected, and made part of the completed building. The two considerations interact. A component may be easy to fabricate but difficult to ship; a connection may be strong but impossible to access after the next component is installed.
DfMA applies at different scales. A team might use it to standardize a family of façade panels, simplify a service rack, coordinate a precast connection, or plan a volumetric module. The broader prefabrication process describes how off-site components fit into project delivery. For the full modular design question, see modular building design.
Core principles of DfMA
Reduce unnecessary variation
Repeated dimensions, connections, and details can make production and installation easier to plan. Standardization is useful when it supports performance and fits the program. It should not be pursued as an end in itself: a standard part that does not fit the building, supply chain, or maintenance plan may create more work than it saves.
Make interfaces explicit
Every component must connect to something. Define the geometry, load transfer, fasteners, seals, service connections, tolerance, access, inspection, and trade responsibility. Interface drawings should make it clear what the manufacturer supplies, what the site team completes, and what evidence proves that the work is accepted.
Design for handling and access
Plan how an element is lifted, turned, supported, protected, stored, positioned, and secured. Consider whether workers can reach the connection with the required tools and whether the work can be checked before it is concealed. Safe and repeatable handling is part of the design, not a detail to invent on installation day.
Coordinate information before release
Manufacturing depends on stable, coordinated information. Establish who approves drawings, what model or dimensions control, how revisions are issued, and how late changes are evaluated. An early design freeze should apply to production-critical information rather than force every finish selection to be made before it is needed.
A practical DfMA workflow
- Set performance criteria. Define function, loads, fire and acoustic requirements, weather exposure, durability, finish, maintenance access, and acceptance tests.
- Select candidate scopes. Look for repetition, difficult site conditions, safety concerns, congestion, or opportunities to inspect concealed work in a plant.
- Engage the supply chain early. Ask manufacturers and installers about equipment, materials, production capacity, tolerances, lead times, transport constraints, and workforce requirements.
- Compare alternatives. Evaluate the same scope as a site-built option, a componentized option, or a larger assembly. Consider cost, schedule, quality, safety, and risk together.
- Simplify the design. Reduce unnecessary parts and unique details, align openings and services, and select a repeatable connection where appropriate.
- Review manufacturing and installation. Walk through the work sequence from raw material to finished assembly, shipment, lifting, connection, inspection, and maintenance.
- Prototype or mock up critical conditions. Test geometry, access, interfaces, appearance, or performance where uncertainty justifies the effort.
- Track results and improve. Record defects, installation time, rework, waste, safety observations, and change causes; use the findings on later production batches.
Examples of DfMA decisions
For a façade, DfMA may group panels into a manageable family, align joints with structure, standardize anchors, and coordinate glazing and insulation in a repeatable sequence. The team still needs to check wind loads, movement, water management, fire requirements, shipping protection, and access for replacement.
For a service rack, the team can coordinate pipe, duct, cable tray, supports, valves, and lifting points before fabrication. The rack may arrive tested as an assembly, but the design must leave access for field tie-ins and maintenance. It also needs to pass through the project’s doors, corridors, shafts, and lifting path.
For a modular room, the design team may align repeated layouts and service zones while keeping module joints accessible. The selected grid must still satisfy occupant needs, structure, egress, transport, and installation. DfMA can reveal that a hybrid approach—prefabricating bathrooms and corridor racks but building the rest on site—is more appropriate than maximizing module size.
Comparing production approaches
| Approach | Manufacturing focus | Assembly focus | Typical DfMA question |
|---|---|---|---|
| Site-built work | Materials, tools, access, sequence, repeatability | Trade handoffs, temporary support, inspections | Can repeated tasks or details be simplified safely? |
| Component prefabrication | Plant process, tolerances, traceability | Handling, connections, installation access | Can the component be shipped and connected without rework? |
| Panelized assemblies | Panel geometry, openings, finishing, packaging | Bracing, joints, weatherproofing, alignment | Are panel edges and openings coordinated with the frame? |
| Volumetric modules | Room-level production, service integration, sequencing | Transport, lifting, stacking, module joints | Does added factory completion justify size and interface constraints? |
Benefits—and the conditions required
When applied early, DfMA may reduce one-off details, make production more predictable, reduce some site operations, and improve access to quality checks. It can also support safer assembly by clarifying handling and sequencing. These are potential outcomes, not automatic savings. A project only realizes them when manufacturing and installation plans are coordinated and the selected scope repeats enough to justify the setup effort.
DfMA may require more effort during early design, earlier supplier engagement, prototype costs, or a longer submittal process before production begins. It can constrain late changes and may create reliance on a smaller number of suppliers. The decision should compare lifecycle performance and installed scope instead of treating reduced site labor as the only measure of success.
Common mistakes
- Assuming DfMA means modular: DfMA can improve a single bracket or service rack without creating a modular building.
- Optimizing for the factory alone: A product still has to travel, be lifted, connected, inspected, and maintained.
- Over-standardizing: Repetition should support the building’s needs, not force an unsuitable layout.
- Inviting manufacturers after design is fixed: Late input can expose constraints when changes are already expensive.
- Ignoring temporary conditions: Lifting and erection can create forces and stability conditions that differ from the completed building.
- Counting only fabrication time: Include engineering, approvals, procurement, production slots, transport, site readiness, commissioning, and contingency.
- Leaving quality evidence vague: Define inspection points, acceptance criteria, unit identification, and nonconformance resolution.
How to evaluate a DfMA proposal
Ask the project team to identify which design decisions change, who supplies each assembly, what is included in the price, and where responsibility transfers. Review a representative detail from production through installation. Check the assumptions behind promised time savings, including site access, labor availability, inspection, weather, and the design freeze date.
Useful project measures can include drawing changes after release, fabrication defects, field rework, installation hours, missed delivery windows, material waste, safety observations, and commissioning deficiencies. Use the measures that connect to the project’s goals. A single headline metric can hide tradeoffs—for example, a faster lift may increase factory rework or require more costly transport.
Worked example: a repeated service corridor
Suppose a project has several floors with similar plumbing, electrical, and ventilation routes. A site-built approach may require crews to measure and install each service run separately while sharing a crowded corridor with other trades. A DfMA review first compares the repeated routes, identifies which supports and clearances can be standardized, and coordinates the rack with beams, corridor ceilings, fire-rated walls, access doors, and branch connections.
The team then asks the manufacturer to price and prototype a representative rack. It confirms the overall shipping length, lift points, protection for exposed ends, access to valves and dampers, and how field joints will be inspected. The contractor tests whether the rack can pass through the route and be lifted into place in the planned sequence. Designers verify that field adjustments do not compromise fire stopping or service clearances. A factory assembly may be selected if its total installed scope and schedule perform well against the site-built alternative. If route constraints or floor-to-floor differences make racks impractical, the team can standardize supports and details while installing the services in the field. DfMA helps make the comparison; it does not predetermine the answer.
The same reasoning applies to façade panels, bathroom pods, precast stairs, or electrical rooms. Define the repeated scope, make the interfaces visible, test handling and installation, and document performance evidence before using the detail on every floor. A limited prototype can expose conflicts at lower cost than repeating an untested condition throughout the building.
Conclusion
DfMA brings manufacturing and assembly considerations into design so that building components can be made and installed with fewer avoidable complications. It works across conventional, prefabricated, panelized, and modular projects. Its value comes from early collaboration, clear interfaces, realistic logistics, stable production information, and performance-based quality planning.
The practical test is to trace one repeated assembly from design through handover. If the team can explain how it will be fabricated, inspected, shipped, installed, connected, and maintained—and compare that plan with a site-built alternative—then DfMA is informing the project rather than serving as a slogan.
Leave a Reply
Want to join the discussion?Feel free to contribute!