Volumetric Modular Construction: Design and Delivery
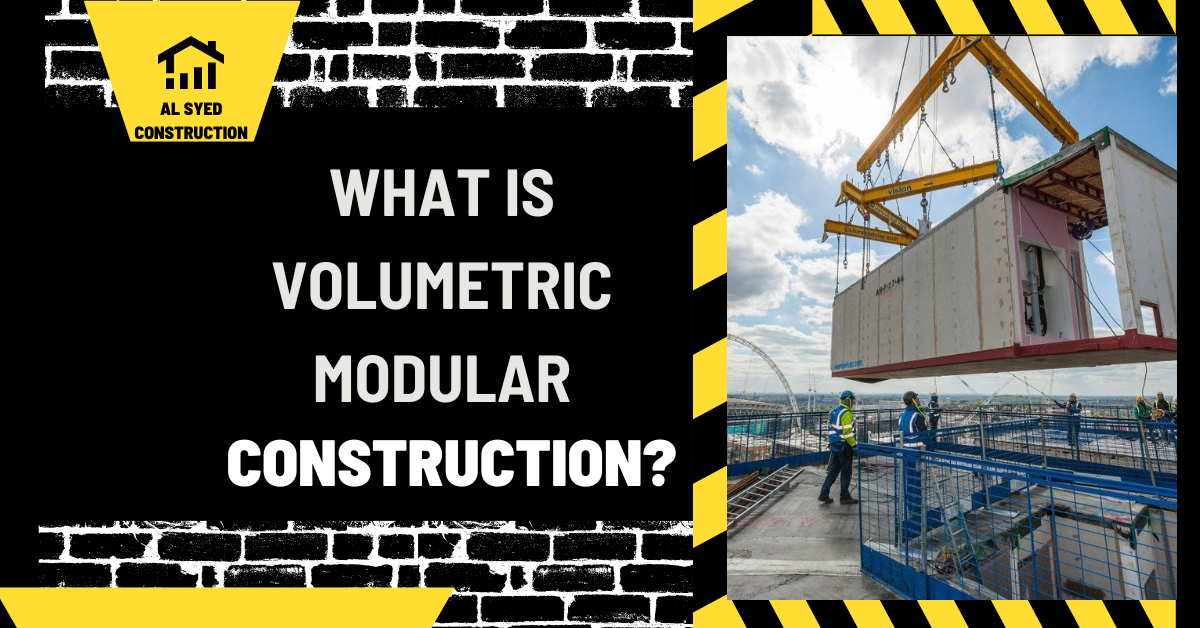
Volumetric modular construction produces three-dimensional building sections in a factory and transports them to the site for assembly. A module may contain a room, a group of rooms, or part of a building floor. Depending on the project, it may arrive with structural framing, walls, windows, finishes, and some building services already installed. The site team then sets the units, connects them, completes interfaces, and tests the building as a whole.
The defining feature is the three-dimensional unit, not a promise that all interior work is complete before delivery. The amount of factory completion varies by project and contract. This guide focuses on the design, transport, stacking, connections, and installation questions that are specific to volumetric modules. For a wider explanation of what “modular” means in construction, see the modular construction definition guide.
How a volumetric system is organized
The building is divided into repeatable boxes or sections that fit together along a planned grid. A module can represent one room, a suite of spaces, or a fraction of a typical floor. Modules may sit side by side, stack vertically, connect to a site-built corridor or core, or combine with panelized and conventional construction. The selected layout depends on the building program, structure, transport, factory capability, and site access.
Because the unit has a floor, walls, and ceiling, it is a structural object both during transport and after installation. The design team must consider the conditions it experiences during lifting, hauling, storage, and setting as well as its final loads. Temporary braces, lifting frames, connection details, and installation sequence should be designed and documented for the actual module.
Volumetric construction is one type of prefabrication. Panelized components use flat assemblies rather than three-dimensional rooms. A project can combine both approaches, for example using volumetric bathrooms and site-built corridors. That hybrid system should have a clear interface so the work is coordinated between manufacturers and field trades.
Establish a module grid around function and transport
Start with the building’s functional plan. Confirm room dimensions, circulation, structural spans, shafts, stairs, bathrooms, kitchens, equipment, and utility routes. The module grid should support the intended use before it is optimized for factory production. A grid that repeats efficiently but produces awkward rooms or blocked circulation is not a successful modular design.
Transport limits then inform the size and configuration of the units. Route width, bridge or weight restrictions, overhead clearance, turning radius, delivery hours, and site access may affect module width, height, length, or shipping orientation. The owner and manufacturer should verify route assumptions early rather than discovering that a completed module cannot reach the site as planned.
Balancing building layout and transport can lead to multiple module types. A typical bedroom module may repeat, while corridor ends, corners, accessible units, mechanical spaces, and façade conditions need unique pieces. The design team should control these variations and show the module identification system on every drawing. For more on how a module grid supports architecture and services, see modular building design.
| Design issue | Volumetric planning question | Risk if unresolved |
|---|---|---|
| Room and corridor layout | Does the grid support furniture, circulation, egress, and daily operations? | Usability problems or costly redesign after production begins |
| Module dimensions | Can each unit travel on the planned route and enter the site? | Transport permit problems, route changes, or a need to split modules |
| Structural system | How do modules bear, stack, brace, and connect? | Unclear load path and field connection rework |
| Building services | Where are risers, utility stubs, access panels, and service zones? | Clashes, inaccessible equipment, or mismatched field connections |
| Enclosure joints | How do air, water, thermal, fire, and acoustic layers cross module seams? | Leaks, sound transfer, or incomplete rated assemblies |
Design the module structure for every stage
Structural design should account for the module’s role in the completed building and the temporary forces during handling. Lifting points, floor stiffness, wall bracing, roof or ceiling framing, and transport restraints need to be coordinated with the manufacturer and responsible engineer. The final design should establish the bearing conditions and connections between modules, foundations, corridors, cores, and site-built components.
Stacking modules introduces vertical interfaces. The design must show how gravity forces pass through the building, how lateral forces are resisted, and what connection sequence is required. End conditions, stair and elevator cores, large openings, and transfer floors may need special coordination. A repetitive stack is only structurally straightforward when its load path and connection details are fully defined.
Foundation supports must align with the module grid and approved reactions. Survey foundation locations and elevations before delivery. The guide to modular foundation systems explains why supports, anchors, and tolerances should be coordinated before setting. If a field dimension is outside the accepted range, obtain written design direction rather than forcing the module or altering a connection.
Coordinate enclosure and interior finishes
Factory completion can include insulation, windows, doors, interior walls, finishes, and services, but the project should state exactly what is included. Exterior finishes can be vulnerable during shipping and lifting. Decide which layers are completed in the factory, which are protected for transit, and which are installed or sealed after modules are connected. The installation drawings should identify the finishing sequence and inspection locations.
Module joints need to preserve continuity of water, air, thermal, fire, and acoustic assemblies. Show details for horizontal and vertical seams, roof transitions, corners, floor edges, and connections to site-built areas. Seals or membranes should be installed on compatible surfaces and inspected before they are concealed. A cosmetic trim strip cannot substitute for a designed enclosure transition.
Interior finishes also need transport protection and a post-delivery inspection process. Doors, glazing, countertops, casework, and floor finishes can shift or sustain damage during hauling. The contract should explain how damage is reported, who determines whether a repair is acceptable, and how the finish warranty applies after setting. Keep records linked to each module number.
Coordinate plumbing, electrical, and mechanical systems
Volumetric modules often contain substantial building services. Kitchens and bathrooms may have factory-installed water and drain lines, ventilation, wiring, and equipment. The utility connection points must align with the site design. Confirm vertical risers, shutoffs, access panels, test points, sleeves, electrical connections, and system labeling before production. The design team should allow enough space to complete connections safely and inspect them.
Mechanical systems need to account for module boundaries. Ducts or piping that cross a seam require a coordinated connection detail and access for testing or maintenance. Equipment location should consider noise, vibration, condensate, service clearances, and replacement routes. Fire and smoke protection around services should be coordinated with the wall and floor assemblies.
Before shipment, perform factory checks of systems within the contract scope and retain records. After modules are connected, test continuity, controls, pressure or leakage where specified, balancing, and system operation. Factory testing can identify issues early, but the entire building must be verified after field connections are completed.
Plan production, transport, and site installation
Production release should follow approved architectural, structural, and MEP drawings. Freeze module types, openings, finishes, equipment, service routing, lifting points, and connections. A change after production begins can affect more than one module and may require new shop work, replacement materials, or revised approvals. Use controlled revisions and a decision log.
Transport planning should use real route data and the actual shipping configuration. Protect modules from weather and road movement, and define staging conditions if they cannot be set immediately. Sequence deliveries in the order needed for erection. Confirm crane capacity and setup conditions through the qualified lift team, and plan exclusion zones, public protection, communication, temporary bracing, and emergency procedures.
During erection, place each module according to the approved set plan. Verify bearings, alignment, elevations, module spacing, and connections as the work proceeds. Maintain temporary stability until the designated permanent connections are complete. The detailed workflow for receiving, lifting, joining, and testing the units appears in the article about modular building installation.
Benefits and constraints
Volumetric construction can shift substantial work away from the site, reduce the number of separate field installations, and help standardize repeated spaces. It may support faster enclosure or reduce disruption at a constrained site when design and site work are coordinated. Factory production can also make some inspections easier before finishes cover the work.
There are real constraints. Transport dimensions can limit room proportions; crane and staging requirements can shape the site; design changes are harder after factory release; and module joints demand careful detailing. The building still needs foundations, utility infrastructure, connection work, site access, inspections, and commissioning. The project schedule only benefits when production, approvals, transport, and site readiness align.
Cost should be compared on total project scope. Include factory work, foundations, transport, cranes, site labor, utilities, enclosure completion, inspections, commissioning, and owner-furnished equipment. A low module quote can exclude substantial site work. The owner should compare equivalent scope and performance rather than judging the delivery method by the unit price alone.
Common problems and prevention
- Designing modules before checking the route: Confirm dimensions, permits, road conditions, and site access early.
- Under-designing the temporary structure: Review handling, lifting, transport, and stacking conditions with the engineer and manufacturer.
- Leaving module joints undefined: Detail structure, enclosure, fire, acoustic, and utility interfaces before production.
- Assuming factory-finished means complete: Write the contract scope for connections, weather seals, testing, and field finishes.
- Setting modules on unverified foundations: Survey supports and clear required inspections before dispatch.
- Skipping post-connection tests: Commission the whole building after services and controls are connected.
Conclusion
Volumetric modular construction uses three-dimensional factory-built units, so design must coordinate the room plan, structure, services, transport, and field connections as one system. The method can bring repeatability and substantial off-site work, but it also places greater importance on early decisions and precise interfaces. A transport-tested layout, approved lifting and connection plans, surveyed supports, protected finishes, and complete post-installation testing help the project deliver a functional building rather than a collection of boxes.
Leave a Reply
Want to join the discussion?Feel free to contribute!